
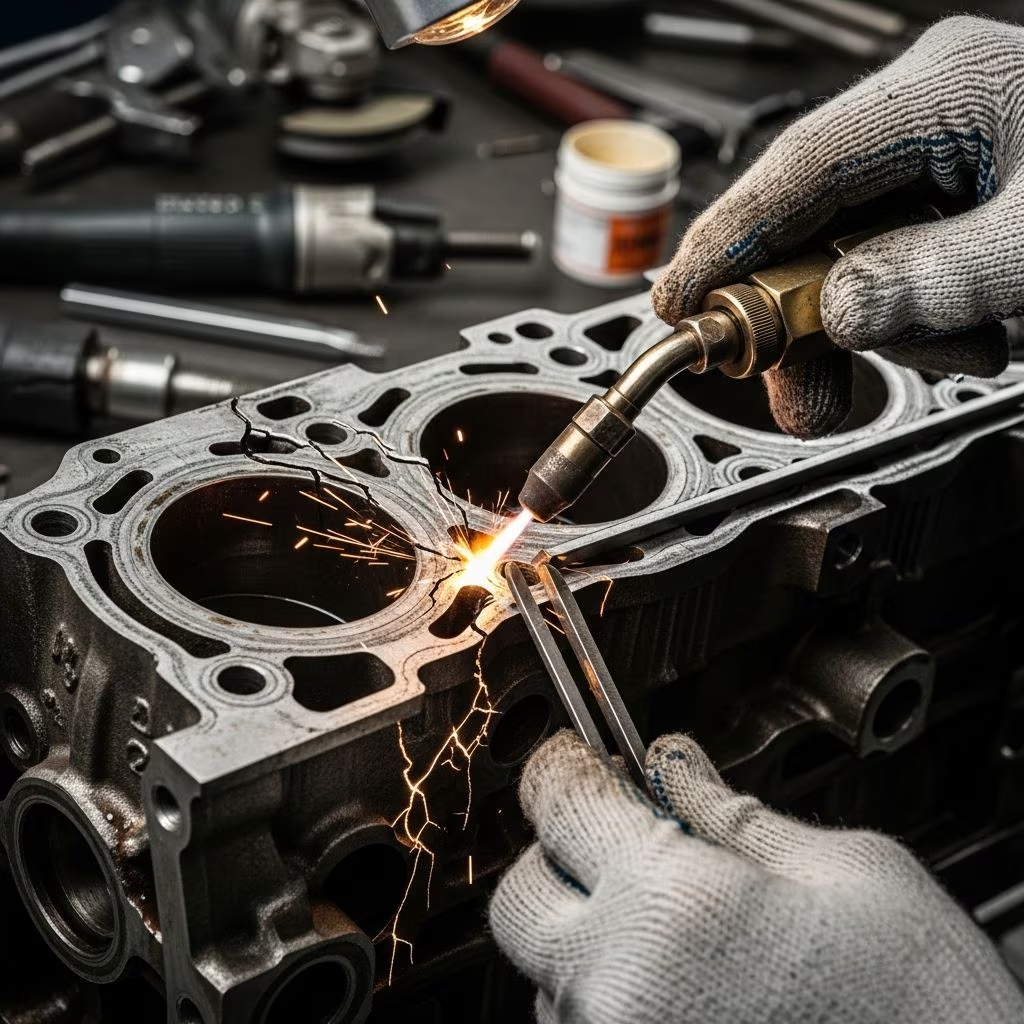
Cracked engine blocks pose a serious challenge for vehicle owners, often leading to coolant leaks, overheating, or complete engine failure. However, with the right techniques, many cracks can be repaired effectively, extending the engine’s life without the need for a full replacement. This guide explores various repair strategies, from simple sealants to advanced mechanical fixes, drawing on established practices used by professionals.
Understanding Engine Block Cracks
Engine blocks, typically made from cast iron or aluminum, endure extreme thermal cycles, pressure, and mechanical stress. Cracks often develop in areas like water jackets, near freeze plugs, or around cylinder walls due to overheating, freezing coolant, or manufacturing defects. Early detection through symptoms such as coolant loss, white exhaust smoke, or oil contamination is crucial.
Small hairline cracks may only affect the cooling system, while larger fissures can compromise structural integrity. Repair feasibility depends on crack location, size, material type, and engine operating conditions. For cast iron blocks, cold repair methods are preferred to avoid heat-induced warping; aluminum blocks may tolerate welding better.
Common Causes of Cracks in Engine Blocks
- Thermal Stress: Rapid heating or cooling cycles cause material expansion and contraction, leading to fatigue cracks.
- Freeze Damage: Water in the cooling system expands when frozen, exerting pressure on block walls.
- Impact or Wear: Physical damage from accidents or prolonged vibration accelerates crack propagation.
- Manufacturing Flaws: Porosity or inclusions in the casting material weaken specific zones.
Repair Method 1: Cold Metal Stitching
Metal stitching, also known as lock-n-stitch, is a popular cold repair technique ideal for cast iron blocks. It involves drilling holes along the crack, inserting tapered or threaded pins, and locking them to pull the crack edges together without applying heat. This method prevents further distortion and is suitable for 80% of cast iron cracks in non-critical areas.
Tools and Materials Needed for Stitching
| Item | Purpose |
|---|---|
| Drill with 3/16-inch bit | Create termination holes and pin sites |
| Threaded stitching pins (iron/steel for cast iron) | Bridge and clamp crack edges |
| Tap set | Thread holes for pin insertion |
| Grinder or die grinder | Vee out crack and roughen surface |
| Spacing tool | Ensure even pin placement |
Step-by-Step Stitching Process
- Inspect and Mark: Use dye penetrant to reveal the full crack extent. Drill small holes at each end to stop propagation.
- Clean Thoroughly: Remove grease, oil, and debris with a degreaser and abrasive cleaning.
- Vee the Crack: Grind a V-shaped groove along the crack to create better pin seating.
- Drill and Tap Holes: Space holes evenly along the crack, tap threads, and insert pins progressively from one end.
- Lock and Trim: Tighten pins to draw edges together; snap off excess and grind flush.
- Final Prep: Pressure test the block after curing to verify seal integrity.
This technique, demonstrated in practical applications on engines like the Toyota 1FZ-FE, provides mechanical strength comparable to the original casting when done correctly.
Repair Method 2: Epoxy and Composite Repairs
For hairline cracks or external damage, high-temperature epoxy compounds offer a straightforward, no-heat solution. Products like metal-filled epoxies bond strongly to cleaned surfaces, restoring pressure resistance in water jackets or bolt bosses. They are especially useful for aluminum blocks where welding risks distortion.
Preparation for Epoxy Application
- Degrease with industrial cleaner to eliminate contaminants.
- Roughen the surface via sanding or blasting for optimal adhesion.
- Vee out and terminate cracks as in stitching.
Application Steps
Mix the epoxy per manufacturer instructions, apply generously over the crack, and reinforce with tape or mesh if needed. Allow 24 hours for full cure before testing. This method has proven effective for industrial engines, saving significant downtime.
Repair Method 3: Welding and Brazing Techniques
When cracks are large or in high-stress areas like near valve seats, welding becomes necessary. Cast iron requires preheating to 500-600°F to prevent new cracks, followed by slow cooling. Aluminum suits TIG welding with inert gas shielding.
Hot Repair Options Compared
| Method | Best For | Pros | Cons |
|---|---|---|---|
| TIG Welding | Aluminum blocks | Quick, strong fill | Requires shielding gas |
| Furnace Welding | Cast iron | Deep penetration | Needs specialized oven |
| Flame Spray | Cast iron cracks/holes | Faster than furnace | Still requires preheat |
| Brazing | Small cast iron cracks | Lower heat | Weaker than welding |
Flame spray uses nickel powder fed into a torch flame, fusing to the crack for durable results. Always match filler material to block composition.
Assessing Repair Viability
Not all cracks are repairable. Reject blocks with cracks through cylinder bores, head gasket surfaces, or main bearing caps. Professional magnaflux inspection confirms damage scope. For high-performance engines, replacement may be wiser despite repair costs.
Preventive Maintenance to Avoid Cracks
- Maintain proper coolant mix to prevent freezing or boiling.
- Monitor for overheating via gauges and regular flushes.
- Use quality gaskets and torque bolts to spec during rebuilds.
- Address vibrations from misaligned mounts promptly.
DIY vs. Professional Repair
Minor external cracks suit DIY with stitching kits or epoxy, costing under $200. Complex internal damage demands machine shop expertise, with repairs ranging $500-$2000 versus $3000+ for new blocks. Success rates exceed 80% for qualified repairs.
Frequently Asked Questions (FAQs)
Can you drive with a cracked engine block?
Short distances may be possible if coolant loss is minimal, but risks escalation to catastrophic failure. Stop driving immediately upon confirmation.
How much does engine block repair cost?
Costs vary: $100-500 for DIY epoxy/stitching, $800-2500 for pro welding, depending on extent and location.
Will a block sealer fix a crack?
Sealants like BlueDevil work for tiny leaks but fail on structural cracks, offering temporary relief only.
Is metal stitching permanent?
Yes, when properly executed, it provides lasting mechanical repair, often outliving the engine if stress is managed.
Can aluminum engine blocks be stitched?
Aluminum stitching exists but welding is more common; use compatible pins to avoid galvanic corrosion.
Case Studies and Real-World Results
Mechanics have successfully stitched cracks near freeze plugs on Land Cruiser engines, enabling full rebuilds. Epoxy repairs on industrial blocks have withstood years of operation. Videos show stitching drawing cracks closed visibly, confirming efficacy.
References
- Engine Block and Head Repair — Engine Builder Magazine. 2015-04-01. https://www.enginebuildermag.com/2015/04/engine-block-and-head-repair/
- How To Repair a Cracked Engine Block — Belzona Blog. Accessed 2026. https://blog.belzona.com/how-to-repair-a-cracked-engine-block/
- Repairing a Cracked Engine Block — Red Power Magazine Community. 2008-04-23. https://www.redpowermagazine.com/forums/topic/38086-repairing-a-cracked-engine-block/
- How to ACTUALLY FIX a CRACKED Engine Block! — RM Garage (YouTube). Accessed 2026.
- Cracked Engine Block Repair — YouTube Video. Accessed 2026.